


Here we only discusses the common carbon steel pipe with diameter less than or equal to 60mm. In the actual welding process of welded pipe, weld cracking is a common welding defect in welding quality problems. The common method is to expand the welded pipe after welding, and the weld directly cracks during the experiment, as shown in the figure below:
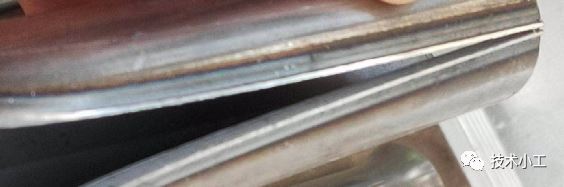
How to deal with this kind of quality problem, we first need to observe the following contents to judge the direction of the problem
1. Whether the width of heat affected zone along both sides of weld centerline on pipe surface is symmetrical; If the width of the heat affected zone along both sides of the weld centerline is inconsistent, it indicates that there is a problem in extrusion forming.
2. Whether the internal and external weld overlap (Burr) of the weld is consistent;
If the weld inside and outside the amount of overlap (Burr) is not consistent, that extrusion molding problems.
3. Whether the neutral line of the weld cross section along the weld position is symmetrical;
If the cross section of the weld is asymmetric along the neutral line of the weld position, it indicates that there is a problem in extrusion forming.
4. After deburring, the color of the weld is heated;
If there is no black luster, only light color, or the heating zone is very narrow, other molding problems can not be seen, most of them are the insufficient heat absorption of the steel strip at the weld.
Generally, the following measures can be taken to deal with the above situations:
1. Adjust the extrusion molding of the extrusion rod
According to the observed quality of the finished product (1, 2, 3 as described above), adjust the matching condition of the extrusion rod and the extrusion amount.
2. Adjust the heating time of heating zone
When to replace the heating coil or adjust the position of coil and extrusion center to ensure enough heating time.


