


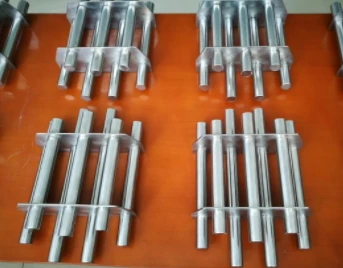
The cross-sectional area of the magnetic rod shall be 70% - -75% of the cross-sectional area of the tube inner diameter. Below 70% results in a significant decrease in efficiency. The rods for high-frequency welded tubes shall have high starting permeability, ua 800 saturated flux density Bs value greater than 3000GS, as high as possible Curie temperature and low loss. In use, it should be noted that the cooling of the magnetic rod should be sufficient to prevent the magnetic rod from crushing or the temperature exceeds the Curie point. The length and position of the magnetic rod will affect the welding efficiency. The above figure shows the specific size of the relative induction ring when welding small, medium and small diameter steel pipes. It should be noted that the total cross-sectional area and length of the magnetic rod used should be adjusted according to the diameter size of the welded steel pipe. Generally, when welding the large-diameter steel pipe, the total length of the magnetic rod may be shorter, but the side of the opening Angle is still beyond the center line of the extrusion roller.


