


High frequency welded pipe unit is the core equipment of the entire HFW production line, and also the equipment with the highest technical requirements of the production line. If it is not adjusted properly, it will directly affect the quality of welded pipe.
We will introduce the common problems and causes of high-frequency welding in detail several times.
1、 External burr shape
External burr is the product of plate edge after high-frequency heating and extrusion. The shape of external burr is affected by welding extrusion amount, welding power, plate edge shape and other factors. Therefore, the shape of external burr is the most intuitive reflection of welding quality, so the welding quality can be judged by the shape of external burr.
Good external burr shape

Part 1 refers to the deformation caused by the strength reduction of the plate edge after heating and the welding extrusion force during welding, which is called deformed metal burr here.
Part 2 is the umbrella shaped bulge formed after the molten metal at the plate edge is melted and the molten metal is extruded. It is called extrusion metal burr here.
The good external burr is that the extruded metal burr is covered on the deformed metal burr in mushroom shape, and is locally fused with the deformed metal burr. The width of weld heat affected zone produced by this condition is moderate.
Flat external burr

The above figure shows flat external burrs. It belongs to overburning phenomenon, which is caused by excessive welding power. Extruded metal burr is covered on deformed metal burr in sheet form, and the burr is flat in overall arc shape, lying on the surface of welded pipe, which is easy to cause excessive width of weld heat affected zone.
Burrs with grooves
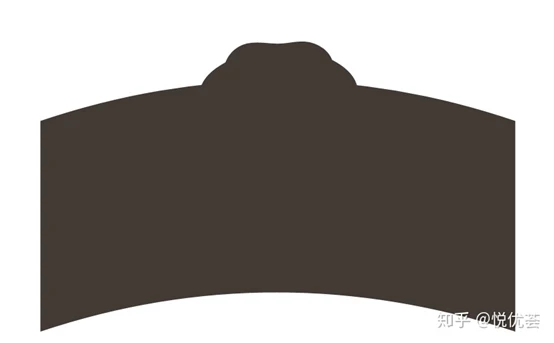 Figure 3
 Figure 4
Compared with Figure 4, Figure 3 shows cold welding caused by too low welding power, and Figure 4 shows cold welding caused by too large extrusion amount.
Generally speaking, with a certain extrusion amount, the higher the welding power, the higher the total amount of external burrs occupied by extruded metal burrs, and the flatter the burr shape; With a certain welding power, the larger the extrusion amount, the higher the share of deformed metal burrs in the total external burrs, and the more upright the burrs are.
The welding extrusion amount is small, and the welding quality can be guaranteed only when the welding power is small; On the contrary, if the welding extrusion amount is large, it requires a large welding power to adapt to it to ensure the welding quality, but too small extrusion amount is not conducive to the elimination of weld inclusions, and too large extrusion amount is easy to cause excessive extrusion of weld molten metal, forming cold welding.
Inclined external burr
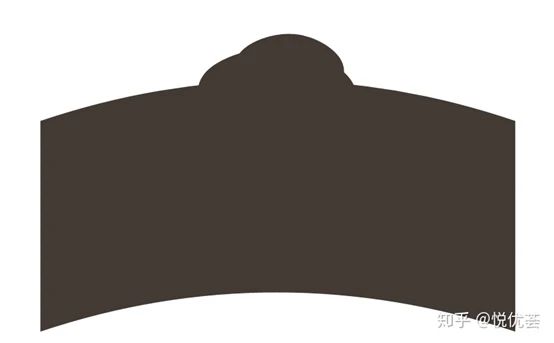
Misalignment exists when two plate edges are connected, which leads to different stress states of the two plate edges, causing the molten metal to deviate from the original position after being extruded


