
Latest Products




Contact Us

CHINA
ADD: ChaoYangNan Str, 300m to BaoCang Express Way Exit, BaoDing, HeBei, China
TEL: +86-312-2090169/2090165
FAX: +86-312-2090165
Email: sales02@metowd.com

IRAN
ADD: No.3 - Golshid9 St. - Nakhlestan Blvd. - Shams abad industrial Zone -40km Tehran Qom Freeway - Tehran - Iran
Postal Code: 1834175977
Tel: 00982156231607-8
Mob: 00989121350509
Email: atiravesh@yahoo.com

Germany Design & Development Office
Germany Design & Development Office
ADD: Wellensiek 111, 33619 Bielefeld Deutschland, Germany
Tel: 0049 521 9890 170
Mob: 0049 163 5149 622


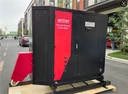
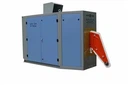
Single Cabinet HF Welder
Product Name: Single Cabinet HF Welder The Single Cabinet HF Welder is the senior type welder compare to Solid State HF Welder. The advantages of the Single Cabinet HF Welder as following: High Efficiency Comparing to traditional solid state welder, save power for 15%-25%. Less Area Covered...
Description
Product Name: Single Cabinet HF Welder
The Single Cabinet HF Welder is the senior type welder compare to Solid State HF Welder.
The advantages of the Single Cabinet HF Welder as following:
High Efficiency
Comparing to traditional solid state welder, save power for 15%-25%.
Less Area Covered
Saving 60% area than traditional solid state welder.
Easy installation
Comparing to the 5-7 days for traditional solid state welder installation, high efficiency switch welder installation is 1 day.
Less installation cost
For example 100kw solid state welder, the traditional welder installation cost is around USD800(purchasing cable, nozzles, cable bridge and brackets), moreover, welder room or elevated platform is necessary, all the cost will be about USD800-1600.
Welding Quality
Benefitted from PWM precise control voltage and three level of filtering, the voltage output is stable, ripple coefficient is 50% lower than solid state welder. The welding quality is obviously better than traditional solid state welder.
20V | 80V | 120V | 150V | 180V | 200V | 235V | |
High efficiency switch welder | 0.65 | 0.9 | 0.94 | 0.95 | 0.96 | 0.96 | 0.96 |
Solid state welder | 0.19 | 0.33 | 0.46 | 0.55 | 0.68 | 0.74 | 0.85 |
Influence of operation on welding quality in high frequency welded pipe production
1 heat input
Because one of the main parameters of welding process, namely welding current (or welding temperature), is difficult to measure, it is replaced by input heat, which can be expressed by oscillator output power
N = Ep·Ip
Where n -- output power, kW;
EP -- screen voltage, kV;
IP -- screen stream, a [1]
When the oscillator, inductor and impedance are determined, the efficiency of the oscillator, output transformer and inductor will be determined. The change of input power is roughly proportional to the change of input heat.
When the input heat is insufficient, the heated edge can not reach the welding temperature, and still maintain the solid structure and can not be welded, forming welding cracks; when the input heat is large, the heated edge exceeds the welding temperature, which is easy to cause overheating, even overburning, and cracking after stress; when the input heat is too large, the welding temperature is too high, which makes the weld breakdown, causing molten metal spatter and forming holes. The suitable welding temperature is 1350 ~ 1400 ℃.
2 welding pressure
Welding pressure is one of the main parameters of welding process. When the two edges of tube blank are heated to the welding temperature, the common metal grains are formed under the action of extrusion pressure, that is, the mutual crystallization and welding. The welding pressure affects the strength and toughness of the weld. If the applied welding pressure is small, the metal welding edge can not be fully pressed, the residual non-metallic inclusions and metal oxides in the weld are not easy to discharge due to the small pressure, the weld strength is reduced, and it is easy to crack after being stressed; when the pressure is too high, most of the metal reaching the welding temperature is extruded, which not only reduces the weld strength, but also produces defects such as excessive internal and external burr or overlap welding. Therefore, the best welding pressure should be obtained according to different specifications. According to practical experience, the unit welding pressure is generally 20 ~ 40MPa.
Because of the possible tolerance of the width and thickness of the tube blank, as well as the fluctuation of the welding temperature and welding speed, the variation of the welding extrusion force may be involved. The welding extrusion amount is generally controlled by adjusting the distance between the extrusion rolls, and can also be controlled by the circumference difference between the front and rear tubes of the extrusion rolls.
3 welding speed
4. Open angle
5 position of inductor and impedance
6. Geometric dimension and shape requirements of tube blank
7 strip edge quality

Why Choose Us:


Hot Tags: single cabinet hf welder, China, manufacturers, suppliers, factory, customized, wholesale, buy, made in China, Inverter Welder, welding machine for experts, welding machine with spot welding function, welding machine for thick wire welding, welding machine for workshop use, welding machine with short circuit protection
You Might Also Like


