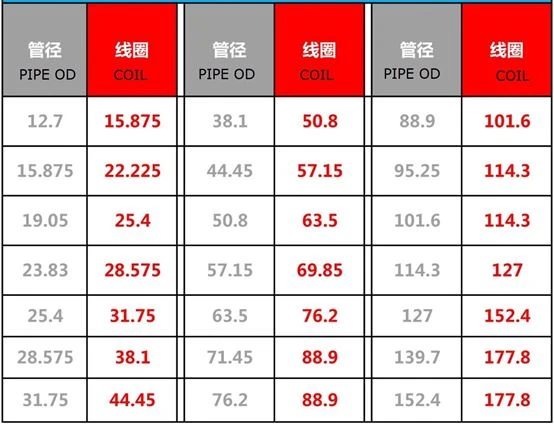
In order to obtain the maximum welding efficiency, it is very important to select the induction coil correctly
The process parameters of high frequency welded pipe production include welding speed (unit speed), welding temperature (high frequency power), welding current (high frequency), extrusion force (die design and material), opening V angle, inductor (coil material, winding direction, position) and size and position of impedance (magnetic rod)
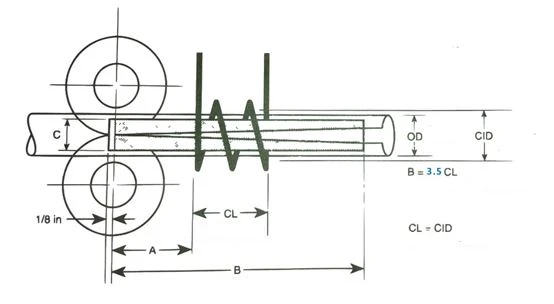
The distance a between coil and extrusion roll depends on the design of rolling mill and extrusion roll diameter. The smaller A is, the better. It is better not to exceed the pipe diameter, as shown in the figure above.
The inner diameter and length of the coil should be equal and about 20% larger than the diameter of the pipe.